Metalizing / Relining Compressor Cylinders
Thermal spray metalizing and sleeve relining to bring worn cylinder bores back to spec, rather than replacing the whole cylinder. This is the same in-house capability shown on our home page — done on our own equipment, on our own schedule.
How We Metalize a Cylinder
Worn bore? We don't just build it back up and hope for the best. There's a process, and we run it the same way every time.
We metalize using a twin arc spray process — two wire electrodes arc against each other, atomizing the metal and depositing it into the bore in controlled passes until we've built the wall back to spec. Once sprayed, it gets machined and honed back to blueprint tolerance — not just "close enough."
Prep is half the job. Before anything gets sprayed, the cylinder is cooked to burn off years of trapped oil and impurities baked into the iron, run through a VAT treatment, then sandblasted to bare, clean metal. Spray doesn't bond to grime — skip this step and the repair doesn't hold, so we don't skip it.
Then we inspect, not guess. Bore measurements get pulled with dial bore gauges to confirm the wear is real and the repair's actually needed. We check the valve seats for wear that calls for facing, and we check the bolt holes for damage that needs to be repaired — helicoil or weld-and-redrill, whatever the hole calls for.
Once we know exactly what it needs, we send you a quote. You approve it, we get the cylinder on the schedule and get to work.
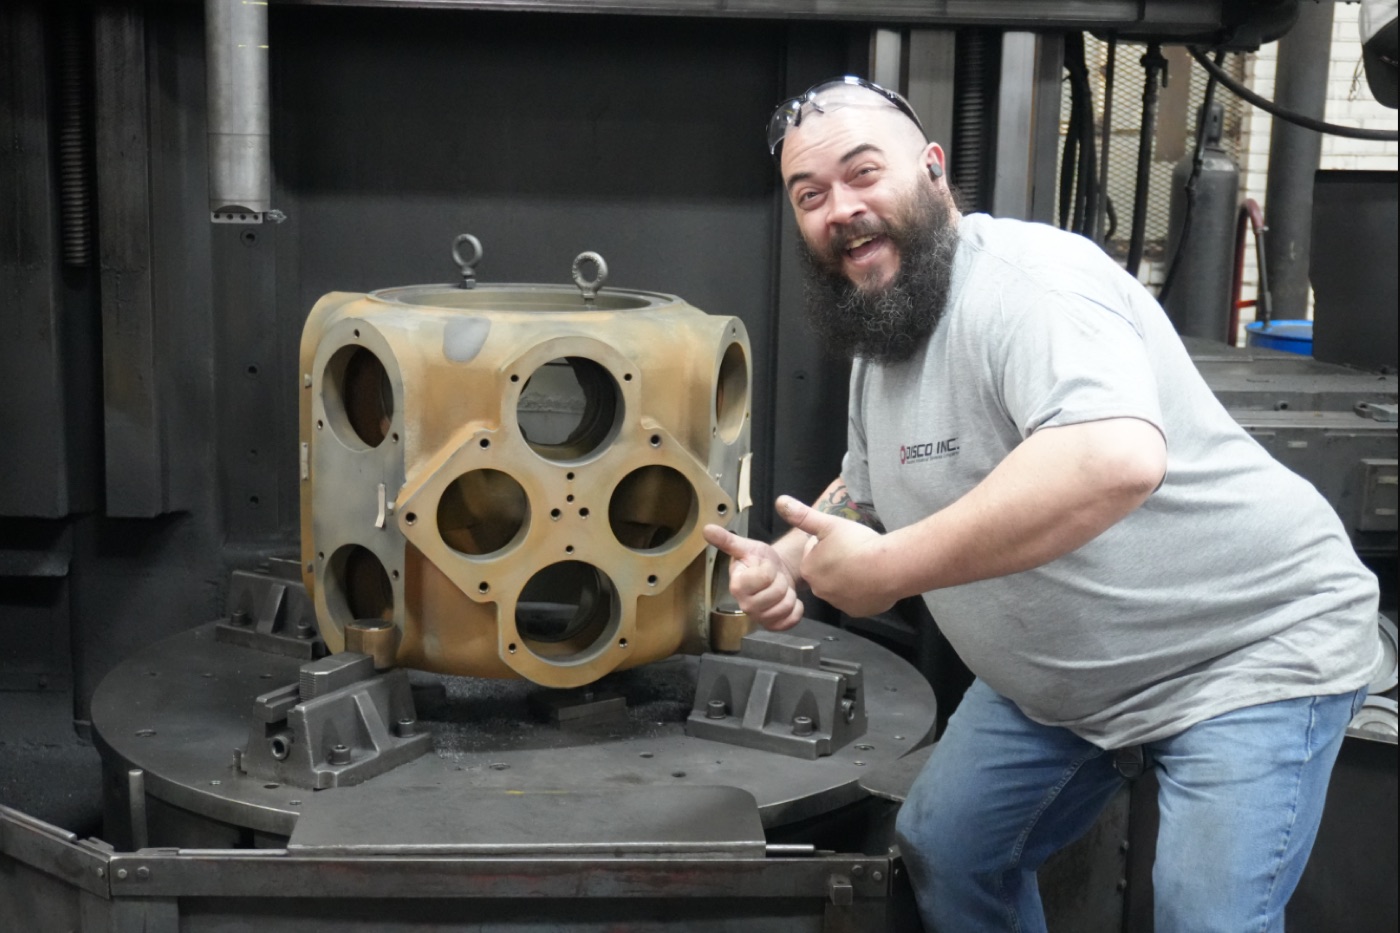
This is Chance. He's been at Disco for a while. If you send a cylinder in to our shop, chances are that he's going to work on it. He loves working on cylinders if you can't tell.
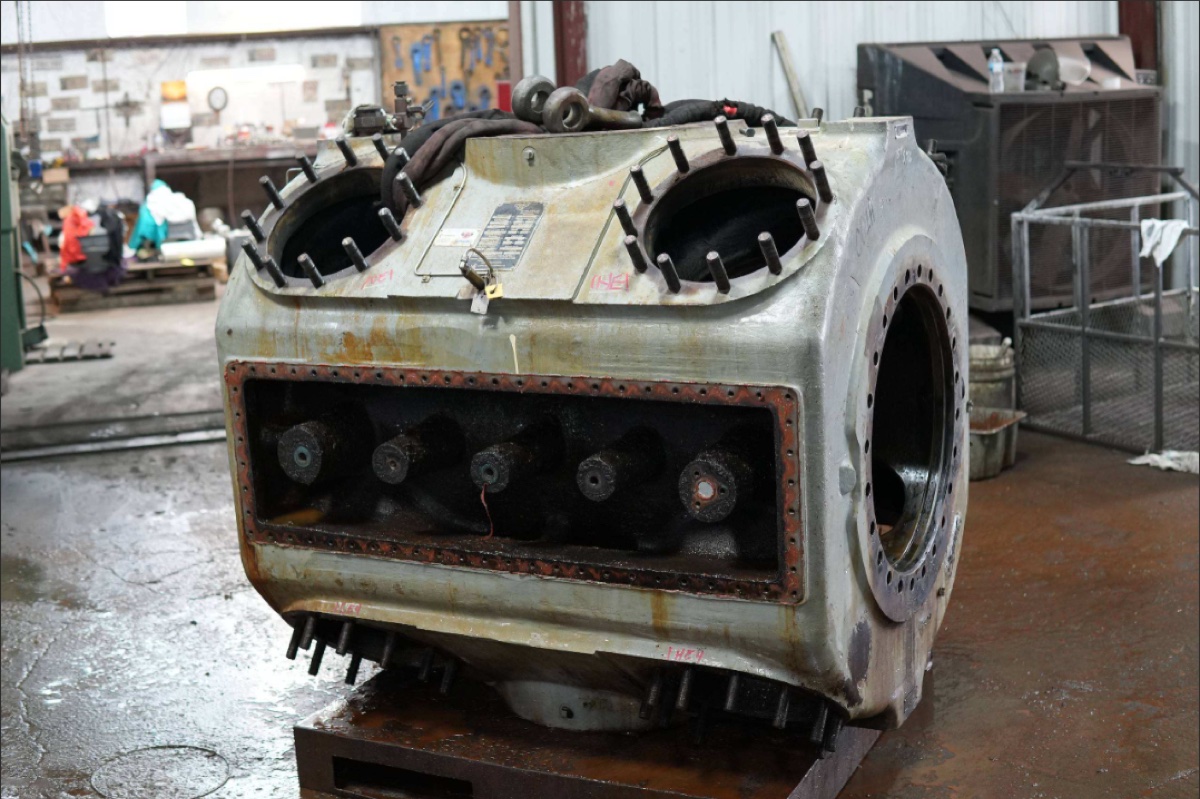
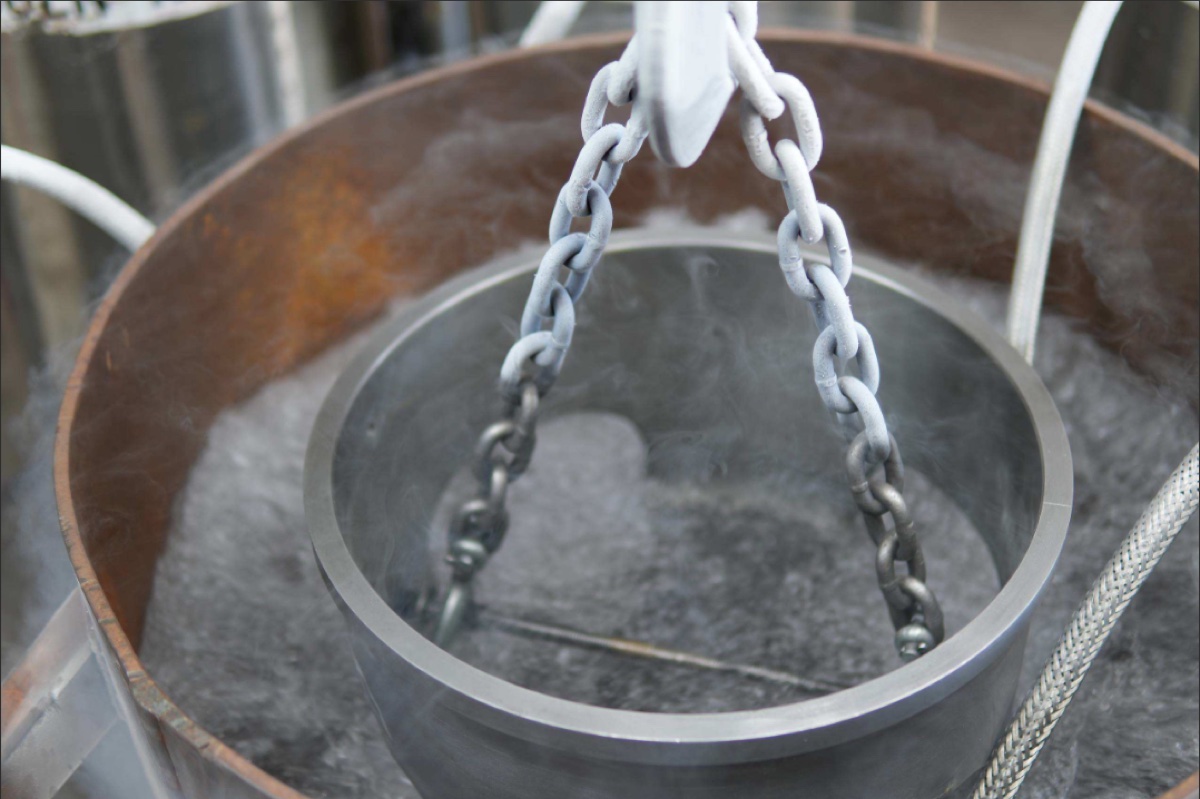
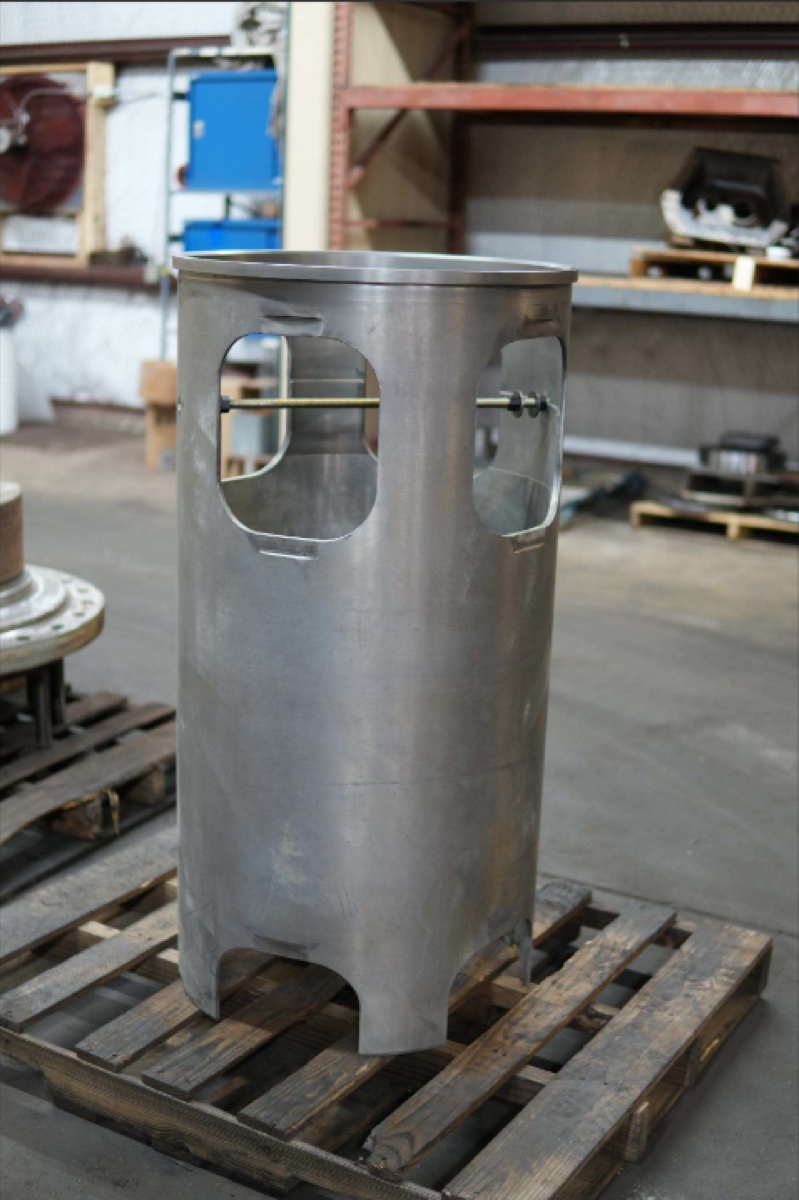
We get a lot of high speed cylinders in to metalize, but we love the opportunity to reline some old iron.
Need a Cylinder Metalized or Relined?
Send us the specs and we'll tell you what it needs.
Request Service